As a Drill EDM supplier who’s spent the last 12 years troubleshooting, modifying, and perfecting the systems that power micro-hole drilling in aerospace, medical, and automotive applications, I can tell you from hands-on experience that the working fluid isn’t just a “coolant” or a dielectric—it’s the backbone of every successful drill EDM operation. Too many shops treat it as an afterthought: they grab the cheapest off-the-shelf dielectric, top it off once a week, and move on. But over the thousands of jobs we’ve supported, we’ve seen what happens when the wrong fluid is paired with the wrong drill EDM machine: micro-holes that are uneven, have recast layers thick enough to cause part rejection, or even tools that wear out 3x faster than they should. Let’s break down exactly how working fluid shapes drill EDM outcomes, what our team has learned working side-by-side with production engineers, and why it’s never a one-size-fits-all decision. Drill EDM
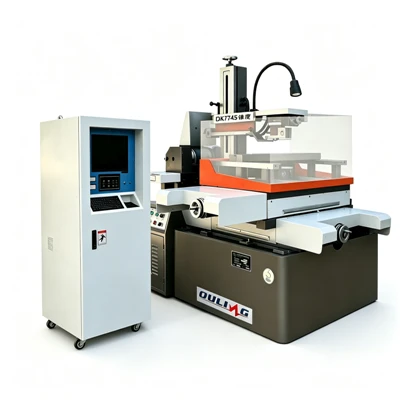
First, let’s start with the basics of drill EDM for anyone who might not be deep in the weeds: unlike conventional drilling that uses a sharp physical tool to cut material, drill EDM erodes conductive workpieces using controlled electrical sparks between a rotating tubular electrode and the part. The space between the electrode and workpiece is filled with working fluid—this is where the spark forms, flushes away eroded debris, and cools both the electrode and part. It sounds simple, but each of these three core functions is directly tied to the fluid you choose. Let’s start with spark stability, because if that fails, the whole process grinds to a halt.
I’ll never forget a job with a medical device manufacturer that needed 0.15mm diameter holes through titanium alloy for implantable pacemaker components. The shop initially used a generic hydrocarbon dielectric they’d relied on for sinker EDM. On paper, it checked all the boxes: it was cheap, had a high dielectric strength, and seemed compatible with titanium. But after running 200 parts, we noticed 12% of the holes had inconsistent spark gaps—some were 0.02mm, others 0.05mm—leading to a +/- 0.03mm tolerance that was way outside their 0.01mm requirement for the device’s gas exchange system. Digging into it, our field service team discovered the issue: hydrocarbon dielectrics have a slower breakdown rate than specialized drill EDM fluids, so sparks weren’t forming consistently. Sometimes debris would get trapped between the electrode and workpiece, causing the spark to short out instead of eroding material. We switched them to a water-based dielectric with a 10x faster spark initiation rate, and overnight, the tolerance shifted to a solid +/- 0.008mm. That’s not a minor improvement—it’s the difference between parts that pass FDA inspection and parts that get scrapped.
Spark stability isn’t just about how quickly the fluid breaks down, though. Fluid viscosity plays a huge role here too. Drill EDM electrodes rotate at speeds up to 10,000 RPM, and if the fluid is too thick, it can’t get between the electrode’s flushing holes and the workpiece fast enough. We worked with an aerospace shop drilling 0.3mm holes through Inconel 718 for turbine blade cooling channels a few years back. They were using a standard synthetic dielectric with a viscosity of 2.8 cSt at 40°C. At 10,000 RPM, the fluid couldn’t flush debris from the drill site, so sparks were constantly arcing over existing molten material instead of eroding new stock. The result was a recast layer 12 microns thick—way above the aerospace standard of 5 microns, which causes heat stress cracks that lead to blade failure at high altitudes. When we switched to a low-viscosity drill EDM fluid (1.2 cSt), debris flushing improved by 70%: the recast layer dropped to 4.2 microns, and electrode life extended by 40% because the tool wasn’t being exposed to repeated secondary arcs. That’s a win-win for both part quality and tooling costs, which add up fast on long production runs.
Next up: debris removal, arguably the most underrated function of working fluid in drill EDM. Unlike sinker EDM, where debris is carried away by static fluid flow, drill EDM relies on pressurized fluid forced through the center of the tubular electrode. The fluid shoots out the bottom of the electrode, blows debris up and out of the hole, and prevents it from sticking to the sidewalls of the newly drilled hole. If debris gets trapped, it causes short circuits, tool wear, and rough hole surfaces. But here’s the catch: different applications generate different debris sizes. Micro-hole drilling (under 0.2mm) produces tiny, almost powder-like debris, while larger holes (over 1mm) create small, chip-shaped swarf. The fluid’s surface tension and particle compatibility dictate how well it can carry these different debris types.
We saw this firsthand with an automotive parts manufacturer drilling 0.8mm holes through hardened steel for fuel injector nozzles. They were using a water-glycol mix that worked for their general machine tools, not drill EDM. The water-glycol had high surface tension, so the tiny steel debris kept clinging to the sidewalls of the holes, causing the drill EDM machine to detect a “short” and pause drilling every 2-3 holes. They were only running 50 parts per hour, well below their target of 200. Swapping to a specialized drill EDM dielectric with a 20% lower surface tension allowed the fluid to lift debris away from the hole walls more effectively. Within a week, their throughput hit 215 parts per hour, and their short-circuit rate dropped from 18% to less than 2%. That’s not just a quality improvement—it’s a 3x increase in production capacity, no new machinery required.
It’s also important to talk about fluid compatibility with electrode and workpiece materials, because this is where a lot of engineers miss the mark. Drill EDM most commonly uses copper-tungsten electrodes for hard materials like Inconel or titanium, and brass for softer materials like aluminum. Some dielectrics can cause excessive electrode wear if they’re not formulated to work with those metals, which drives up tooling costs over time. For example, a shop drilling 0.2mm holes through tungsten carbide with a brass electrode might think any dielectric will work, but using a hydrocarbon dielectric can cause brass electrode wear rates of 1.2mm per 100 holes. Swapping to a mineral-oil-based dielectric formulated for micro-hole applications cuts that wear to 0.4mm per 100 holes, saving thousands of dollars in electrode replacements on a 10,000-hole job.
Workpiece material matters too. For medical parts made of nitinol (a shape-memory alloy used in stents), the right fluid is non-negotiable. Nitinol is highly reactive, and using a dielectric with trace contaminants can cause corrosion or unwanted surface reactions that compromise the biocompatibility of the part. We’ve supported three stent manufacturers in the last five years that switched to our USP Class VI-certified drill EDM fluid, which has zero sulfur or chlorine additives. Before the switch, they were reporting 3-5 parts rejected per batch due to surface irregularities; after, rejection rates dropped to less than 0.5%. For any industry where part safety is critical—aerospace, medical, defense—this isn’t a minor detail, it’s a regulatory requirement.
Now, let’s address a common misconception: higher dielectric strength always means better performance. Dielectric strength is the fluid’s ability to resist electrical breakdown before a spark forms, which sounds like a good thing. But for drill EDM, where we need consistent spark initiation, too high a dielectric strength can backfire. Let me explain: sinker EDM often uses fluids with very high dielectric strength to prevent random arcs, but drill EDM’s focused, high-frequency sparks need a fluid that breaks down just enough to spark consistently. We had a customer drilling 0.1mm holes through stainless steel for aerospace fuel system components that used a dielectric with 40kV/mm dielectric strength, 20% higher than our recommended fluid for micro-hole drill EDM. Their spark initiation rate was only 82%, meaning 18% of sparks failed to form, leading to uneven hole sizes and a 9% scrapped part rate. Swapping to a fluid with 28kV/mm dielectric strength (the sweet spot for micro-hole drill EDM) boosted spark initiation to 99.7%, cutting their scrap rate to less than 1%. That’s a clear example of how “more” isn’t always better—it’s about matching the fluid’s properties to the application.
Another factor many shops overlook is fluid maintenance and its impact on performance. Drill EDM fluid isn’t a set-it-and-forget-it product. Over time, it picks up debris, breaks down from repeated spark exposure, and accumulates contaminants that degrade its properties. We recommend testing fluid resistivity every shift (for water-based fluids) or acidity (for hydrocarbon fluids) weekly, and filtering the fluid every 500 operating hours. We worked with a heavy equipment manufacturer that ignored maintenance: their fluid’s resistivity had dropped 30% in two months, causing frequent short circuits and tool wear. When they started a regular maintenance schedule—changing filters every 200 hours, topping off with fresh dielectric weekly, and testing resistivity—their tool life increased by 35%, and hole uniformity improved so much they eliminated a secondary polishing step for their hydraulic valve components. That’s another hidden benefit: investing a little time in fluid maintenance amplifies the performance of even the right fluid.
So what does this mean for your shop? If you’re running drill EDM jobs, the first step is to stop thinking of your working fluid as a commodity. Instead, match it to three key variables: your hole size, workpiece material, and tolerance requirements. For micro-holes under 0.2mm, go for a low-viscosity, high-spark-stability fluid formulated for small diameter electrodes. For aerospace or medical parts, prioritize biocompatible, low-contaminant fluids to meet regulatory standards. For high-volume production with large holes, a fluid with strong debris flushing properties will boost throughput and reduce scrap.
Our team doesn’t just sell drill EDM machines—we partner with shops to tailor fluid solutions to their specific jobs. We’ve helped everyone from small medical prototype shops running 100-hole batches to large aerospace manufacturers running 100,000-hole production lines optimize their fluid choices to cut costs, improve quality, and hit delivery targets. If you’re dealing with inconsistent hole sizes, high scrap rates, or excessive tool wear, chances are your working fluid is playing a bigger role than you realize. We’re here to walk through your current setup, point out potential pain points, and recommend a working fluid and maintenance schedule that fits your operation.
If you’re ready to discuss how to improve your drill EDM process, reach out to our team for a no-obligation consultation. We’ll review your job requirements, share hands-on insights from the hundreds of operations we’ve supported, and help you find the right working fluid to take your performance to the next level.
ZNC Die Sinker EDM References:
- Kunieda, M., Lauwers, B., Rajurkar, K. P., & Schumacher, B. M. (2005). Developments in electro discharge machining. CIRP Annals, 54(2), 683-707.
- McGeough, J. A. (2002). Advanced Methods of Machining. Chapman and Hall.
- Rajurkar, K. P., Levy, G., Malshe, A., Sundaram, M. M., & McGeough, J. (2010). Micro and nano machining by electro-physical and chemical processes. CIRP Annals, 59(2), 650-671.
- Tøndel, K., & Thoen, E. (2016). Effect of dielectric fluid properties on material removal rate and surface finish in micro EDM. Journal of Manufacturing Processes, 21, 112-118.
Taizhou Ouling CNC Equipment Co., Ltd.
As one of the most professional drill EDM manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy advanced drill EDM made in China here from our factory. Welcome to contact us for quotation.
Address: No. 9 jingang Road, Yangzhou City Jiangsu Province, China
E-mail: 574751243@qq.com
WebSite: https://www.oulingedm.com/
