If you’ve ever stood next to a hood furnace during a production run—maybe at a metal treating shop, a ceramics lab, or a semiconductor fab—you’ve probably noticed that first, there’s that loud roar of exhaust pulling air through the system, and second, there’s a very specific reason the operators watch a small pressure gauge like it’s a lifeline. As someone who’s spent 12 years selling and troubleshooting hood furnaces, I can tell you: pressure isn’t just a number on a gauge. It’s the quiet, invisible hand that guides every part of your process, from part quality to energy bills, and even the safety of your team. Most of the problems we get called about aren’t from broken heating elements or worn insulation. They start when a customer misadjusts pressure—too high, too low, or just wrong for their load—and by the time they notice, they’ve wasted hundreds of pounds of metal, ruined a batch of high-value parts, or missed a deadline. Let me break down how this works, from the small-batch sintering jobs we do for medical device makers to the big vacuum hood furnaces for aerospace components. Hood Furnace
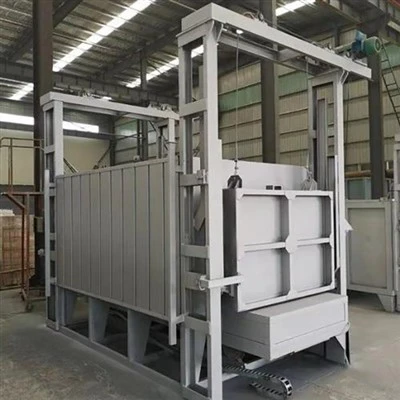
First, let’s get the basics straight, because most new operators mix up the two pressure zones around a hood furnace: inside the work chamber, and inside the hood itself (the big metal cover that seals over the chamber and connects to the exhaust system). The chamber is where your parts sit, being heated, cooled, or treated. The hood is the system that controls the air flow around that chamber. Pressure here is measured in “inches of water column” (in WC) or Pascals, which sounds fancy but is just a way to measure how hard air is pushing against a surface. For context, the atmospheric pressure around us every day is about 14.7 pounds per square inch, or 407 in WC—so the pressure we care about for furnaces is a tiny fraction of that, usually between -0.5 and -5 in WC for most jobs. The minus sign is important: it means the furnace is operating under negative pressure, not positive. I see a lot of first-time customers crank up the exhaust to make sure no fumes leak out, only to accidentally push the chamber into positive pressure, and that’s where the trouble starts.
Let’s start with the most obvious impact: part contamination. This is the reason we stress pressure adjustment more than any other setting. If your hood furnace is operating at positive pressure inside the chamber—meaning air is pushing out, not pulling in—any gaps in the chamber seals, door gaskets, or even small cracks in the furnace lining will suck in whatever is around the furnace. If you’re in a machine shop, that’s metal shavings, oil mist from cutting fluids, or dust from grinding operations. If you fire ceramics, that’s kiln dust or leftover glaze splatter. If you’re doing heat treating for aerospace, that’s airborne hydrocarbons from nearby equipment, or even moisture in the plant air. Last year, a customer in Detroit called us panicking—they had a batch of stainless steel turbine blades that came out with tiny black spots on the surface, ruining a $12,000 run. When our service tech checked, they found the furnace’s exhaust fan had been replaced a month earlier, and the new fan was too strong, pulling the chamber into positive pressure. It was sucking in dust from the warehouse floor through a small crack in the chamber door gasket. We adjusted the pressure to -1.2 in WC, replaced the gasket, and their next batch was perfect. That’s not an isolated case. We get at least one call a quarter about contamination linked to pressure misadjustment, and it’s almost always positive pressure.
Negative pressure, by contrast, works the way it’s supposed to: it pulls air out of the chamber, so nothing gets in. The key is getting that negative pressure just right, not too high or too low. Too much negative pressure—say, -4 in WC or higher—can cause its own problems. Let’s talk about gas flow first. If you use a hood furnace for processes like sintering, brazing, or annealing, you often flow a protective gas (argon, nitrogen, or forming gas) through the chamber to prevent oxidation. If your exhaust is pulling too hard, it can suck all that protective gas out before it does its job. I had a customer in Boston who was sintering titanium parts for hip implants. They were using nitrogen gas, but they’d cranked the exhaust to get rid of a small amount of moisture, and ended up pulling so much nitrogen through the chamber that the titanium oxidized mid-sinter, turning a shiny gray part dull and brittle. Our tech calibrated the pressure to -1.5 in WC, and they cut their nitrogen usage by 22% that month, while improving part quality. That’s a double win: better parts and lower utility bills.
For processes that require a controlled atmosphere—like heat treating steel to get the right hardness, or annealing copper to make it malleable—uniform pressure is everything. If pressure fluctuates during a run, you get uneven treatment. Let’s take annealing steel: if one part of the chamber has a slightly lower pressure, oxygen can sneak in, making that part of the steel harder or more brittle than the rest. If pressure spikes, it can blow small gaps in the protective gas layer, leading to inconsistent results. We once built a hood furnace for a job shop in Chicago that ran small batches of tool steel for cutlery. Their first few runs had a 15% rejection rate due to uneven hardness. The problem? They were using a manual damper on the exhaust, and the pressure would drop by 0.8 in WC every time they opened the door to load parts. We added a variable speed exhaust fan and a pressure controller that adjusts automatically, keeping the pressure within ±0.1 in WC for the entire run. Their rejection rate dropped to 2% that quarter. That’s a huge difference for a shop that runs 50 batches a week.
Now, let’s talk about energy efficiency, which is a big one for any manufacturer. Most people don’t realize that pressure directly affects how much energy your hood furnace uses. If you’re running at too high a negative pressure, you’re pulling more air through the chamber than you need. That air has to be heated, or it has to be exhausted, and your furnace has to work harder to maintain its set temperature. We did a test last year with a customer in Cleveland who ran a medium-sized hood furnace for stress relieving aluminum parts. Their energy bill was $1,800 a month for the furnace. We adjusted their pressure from -3.2 in WC to -1.5 in WC, and within a month, their energy bill dropped to $1,420. That’s a 21% reduction, just from fixing pressure. Why? Because too much exhaust air was being pulled out, and the furnace’s heating elements had to run longer to keep the chamber at 1,100 degrees Fahrenheit. When we brought pressure to the optimal range, the protective gas stayed in the chamber, the heat didn’t get pulled out unnecessarily, and the elements ran more efficiently. We’ve seen similar savings across industries—from 15 to 25% energy reduction just by calibrating pressure right.
Safety is another area where pressure makes a huge difference, and it’s something we never downplay. For furnaces that use flammable gases—like hydrogen for brazing, or natural gas for high-temperature heat treating—positive pressure is a massive fire hazard. If you have a gas leak, positive pressure will push the gas out into the shop, creating an explosive atmosphere. I’ve been on a site where a customer had a small hydrogen leak because their pressure was accidentally set to positive, and by the time our tech arrived, the gas detector was going off every few minutes. It was a lucky break that nobody was working near the furnace at the time. Negative pressure, on the other hand, contains those gases, pulling them straight into the exhaust system where they’re burned or vented safely. Even for non-flammable processes, pressure affects operator safety: too much negative pressure can make the door hard to open, leading to injuries when operators yank it open too fast, or even blow back hot air if the pressure spikes suddenly. We include pressure interlocks on every hood furnace we sell—meaning the furnace won’t heat up if pressure is outside the safe range—to prevent these issues before they happen.
One common question we get is: does pressure matter for every type of hood furnace? The short answer is yes, but the optimal pressure changes based on your process, the type of parts you’re running, and the furnace’s design. Vacuum hood furnaces, which we use for high-temperature aerospace and medical parts, operate at much lower pressures—sometimes as low as -29 in WC (near full vacuum) because those processes require zero air to prevent oxidation. For lower-temperature processes, like annealing or drying parts, we usually recommend -1 to -2 in WC. For processes that release more fumes—like degreasing parts with oil before heat treating—we might go a bit higher in negative pressure, around -2.5 in WC, to pull those fumes out faster. The key is that there’s no one-size-fits-all number, which is why we include free process testing with every furnace we sell: we send a tech to your shop, run a small test batch on your actual parts, and dial in the exact pressure and other settings that work for your operation.
I’ll be honest: this is one of the biggest mistakes we see new buyers make. They buy a hood furnace, get it installed, and just use the default pressure setting the manufacturer listed in the manual. But that manual setting is a baseline, not a solution for your specific shop. A job shop running small batches of tool steel has different pressure needs than a semiconductor fab running silicon wafers, which have to be completely free of even tiny particles. Last year, we had a customer who bought a used hood furnace from an online auction, and the previous owner had run it for ceramics. He tried to use it for heat treating, and his parts kept oxidizing. When our tech checked, the furnace’s pressure controller was calibrated for ceramics, not metal, and it was set to -0.8 in WC—too low to pull enough protective gas through the chamber for heat treating. It took 10 minutes to adjust the controller, and his next batch was perfect. That’s how small a change makes such a big difference.
So, what should you take away from all this? Pressure isn’t a trivial setting on your hood furnace. It impacts part quality, energy costs, operator safety, and even your bottom line. Too little negative pressure, and you get contamination, uneven treatment, and ruined parts. Too much negative pressure, and you waste gas, energy, and time. Positive pressure is a ticking time bomb for fires, contamination, and safety incidents. The good news is that this is a fixable problem. Whether you’re looking to replace an old furnace with a new, pressure-controlled model, or just want to get better performance out of the one you have, getting pressure right is the first step to better, more efficient operation.
If you’re tired of wasting parts, overpaying for energy, or dealing with quality issues that pop up for no clear reason, we can help. We’ve installed hood furnaces for metal treating shops, ceramics labs, medical device manufacturers, and aerospace parts makers across the country, and we know how to tailor pressure settings to your exact process. We offer free process assessments, on-site calibration, and ongoing support to make sure your furnace runs at its best, not just at the default settings. Don’t let a simple pressure setting derail your production. Reach out today to discuss your needs, and let’s work together to get your hood furnace operating at peak efficiency.
Car-Bottom Forging Furnace References
- Davis, J.R. (Ed.). (2005). Heat Treater’s Guide: Practices and Procedures for Irons and Steels (2nd ed.). ASM International.
- Boyd, D., & Patel, R. (2018). Furnace Atmospheres: Control and Application for Industrial Processes. Industrial Press Inc.
- American Society of Safety Professionals. (2020). Safety Guidelines for Industrial Furnace Operations. ASSP.
- Kim, S., & Lee, H. (2021). Pressure Control Optimization for Sintering Processes Using Industrial Hood Furnaces. Journal of Manufacturing Processes, 67, 412-421.
- Smith, T.L. (2019). Energy Efficiency in Industrial Thermal Processing: Reducing Costs and Emissions. CRC Press.
Danyang Dingfeng Industrial Furnace Co., Ltd.
Danyang Dingfeng Industrial Furnace Co., Ltd. is one of the most experienced hood furnace manufacturers and suppliers in China, also supports customized service with low price. Please feel free to wholesale high quality hood furnace made in China here from our factory. For pricelist, contact us now.
Address: Lizhuang Economic Development Zone, Danyang City
E-mail: saleszk@dffurnace.com
WebSite: https://www.dffurnace.com/
